

Laser welding is mainly aimed at the welding of thin-walled materials and precision parts. The welding process belongs to the heat conduction type, that is, the laser radiation heats the workpiece surface, and the surface heat diffuses internally through heat conduction. By controlling the laser pulse width, energy, peak power and repetition frequency and other parameters, the workpiece is melted to form a specific molten pool.Laser welding is a new welding method, and also one of the important aspects of the application of laser material processing technology. Laser welding is mainly aimed at the welding of thin-walled materials and precision parts. The welding process belongs to the heat conduction type, that is, the laser radiation heats the workpiece surface, and the surface heat diffuses internally through heat conduction. By controlling the laser pulse width, energy, peak power and repetition frequency and other parameters, the workpiece is melted to form a specific molten pool.
Product advantages
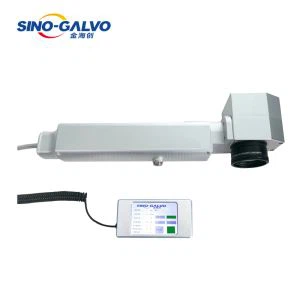
- Hand-held laser welding machine, with a new generation of hand-held welding head to replace the traditional fixed light path, flexible and convenient, overcome the limitation of work table space, work size is not unified when the situation can not automatically welding. Mainly for large workpiece fixed position such as inside right Angle, outside right Angle, plane weld welding.
- Small heat affected area, small deformation, and welding depth, welding firm, it is a new welding technology for long-distance welding large parts.
- Laser welding can weld hard to reach parts, non-contact remote welding, with great flexibility.
Technical parameters
| Laser/Welding system/Cooling system Parameters | |||
| Laser | |||
| Power | 1500w | 2000w | 3000w |
| Power supply | 220v | 220v±10 | 380v±10 |
| Laser wavelength | 1080±5nm | ||
| Working methods | Continuous / Modulated | ||
| Welding speed | 0.7-2.0 / min | ||
| Working environment temperature | -5℃ to 35℃ | ||
| Working environment humidity | <70% no condensation | ||
| Cooling system | water cooling | ||
| Machine power | ≥ 6KW | ≥ 8KW | ≥ 10KW |
| Welding System | |||
| Wire feeder | Including | ||
| Applicable power range | 0 to 2000w | 0 to 2000w | 0 to 3000w |
| Applicable welding gap width | ≤ 3mm | ≤ 3mm | ≤ 8mm |
| Applicable welding materials | Carbon steel, copper alloy, aluminum profiles, galvanized sheets, stainless steel, gold, silver, etc. | ||
| Cooling System | |||
| Industrial Water-Cooling | Optional (S&A, Hanli or others) | ||
| Model | SCH-1500C or others | SCH-2000C or others | SCH-3000C or others |
| Power supply | 220V 50HZ | ||
| Refrigerant | R410A | R32 | R32 |
| Power | 2.1KW | 2.5KW | 3.5KW |
| Working temperature | -5℃ to 35℃ | ||
| Environment humidity | <70% | ||
| Control method | Panel control | ||
Main application

Laser Welding Machine is mainly used for laser welding of pulling metal, chassis and water tank;
Laser welding of all kinds of metal lighting frame;
Laser welding of stainless steel doors and Windows, aluminum doors and Windows;
Stainless steel bathroom, kitchen cabinet laser welding;
Billboard, advertising word laser welding.
Self-checking and FAQ
|
Common faults |
Fault description and solution measures |
Handler |
|
The whole machine cannot be powered on |
1. If the device fails to be powered on, check whether the power supply cable is normal, and then check whether the circuit breaker, emergency stop, and power button are pressed. 2. Check whether the latching relay is normal or not. If it is damaged, it can be replaced by itself or reported after sale. 3. If the enable light is not on, the enable button is damaged and can be replaced for testing. 4. The wiring contact of the enable button is poor |
Trained personnel |
|
Laser alarm |
1. Check whether the cooling water alarm causes the machine before the laser alarm, and check whether the water tank is turned on or gives an alarm. 2. Qbhfth alarm, which is caused by loose installation of optical fiber head and collimation. It needs to be reported to the after-sales personnel for handling. 3. The laser water circulation is blocked and there is gas in the cooling water pipe. Check the water circulation and discharge the air in the water pipe. |
After-sales personnel |
|
Not light |
1. When the laser does not emit light, first check whether the laser is turned on. When the red light is emitted from the gun head, whether the laser gives an alarm and whether the enable light on the laser panel is on. 2. The red light is not emitted from the gun head, the laser does not give an alarm, and the enabling lamp is normal. It may be that the swing lens is damaged and needs to be replaced by after-sales personnel. 3. The red light is emitted from the gun head normally, and the laser does not give an alarm. If the enable light is pressed, the enable light on the laser panel does not light up, it may be that the laser expires. You need to connect the laser with a computer to check whether the laser control is in the external control mode, and then enter the password. All the above are normal. Check whether the safety lock of the touch screen is opened and whether there is a connection between the gun head and the grounding wire when it is opened. |
After-sales personnel |
|
Laser weakening |
1. When the laser becomes weak, first confirm whether the red light is emitted in the middle of the gun. 2. Whether the protective lens is damaged and whether the protective gas is turned on. 3. Whether to weld on the focus. 4. If the above are normal, connect the laser with the computer to monitor whether the current laser power is consistent with the set power in real time. 5. If the power setting is normal, it is necessary to check whether the focusing lens and optical fiber head are damaged, which needs to be handled by after-sales personnel. |
After-sales personnel |
|
Protective lenses are vulnerable |
1. When the protective lens is damaged frequently during welding, check whether the gas is turned on. 2. Whether the current power is adjusted to the maximum. When the laser power increases to more than 90%, it is recommended to use defocus welding to avoid damage to the protective lens caused by excessive spatter. 3. During welding, the gun head and the working surface shall be welded between 0-65 degrees ,avoid 90 degrees between the laser and the working surface (special attention shall be paid when welding aluminum alloy materials). |
Trained personnel |
|
Water tank alarm |
1. High temperature causes an alarm. When it occurs, first turn off the power supply of the whole machine and check whether the exhaust outlet behind the cabinet is blocked, resulting in excessive temperature of the water tank. 2. The abnormal water flow causes the alarm. The water flow alarm is generally the bending of the water pipe. You can check whether the water pipe is bent. |
Trained personnel |
Hot Tags: sino galvo laser welding machine for sale, China, suppliers, manufacturers, customized, low price, application of